The short answer: you handle variable raw material loads by building slack into the system before the material ever hits your cooker — not by hoping the flow stays steady. That means oversized buffer capacity, flexible conveying speeds, and a scheduling mindset that treats intake volume as a variable, not a constant. Plants that skip this step end up rationing capacity on the busiest day of the week and running half-empty cookers on the slowest — both are expensive mistakes.
Why Rendering Plants Almost Never See a Flat Intake Curve
Ask any plant manager what Monday looks like compared to Thursday, and you’ll usually get a shrug and a number that’s off by 30-40%. Slaughterhouses don’t kill the same volume every day. Feed mills processing feather meal or meat and bone meal get shipments in erratic batches. Biodiesel producers sourcing used cooking oil and animal fats deal with supply that shifts by season and by contract renewal.
Add in disease outbreaks, holiday demand spikes for meat, and weather disruptions to transport, and you get intake swings that can hit 50% above baseline on a bad week. A plant designed for the average day chokes on the peak day — and that’s when odor complaints, equipment strain, and quality drops all happen at once.
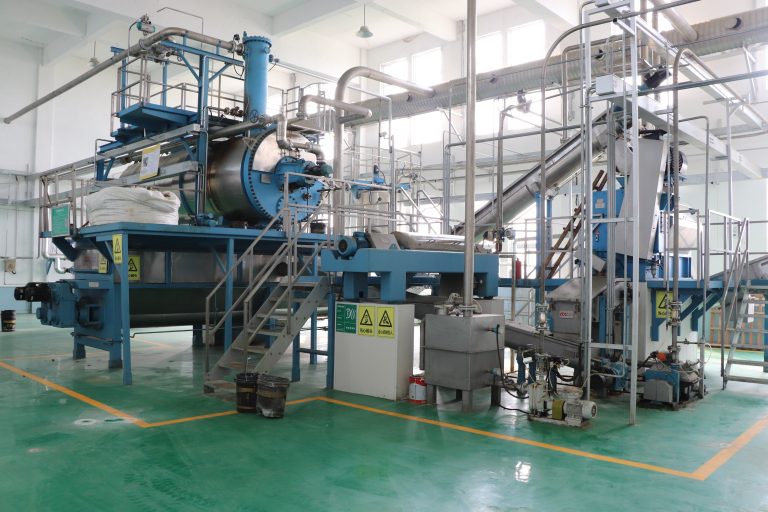
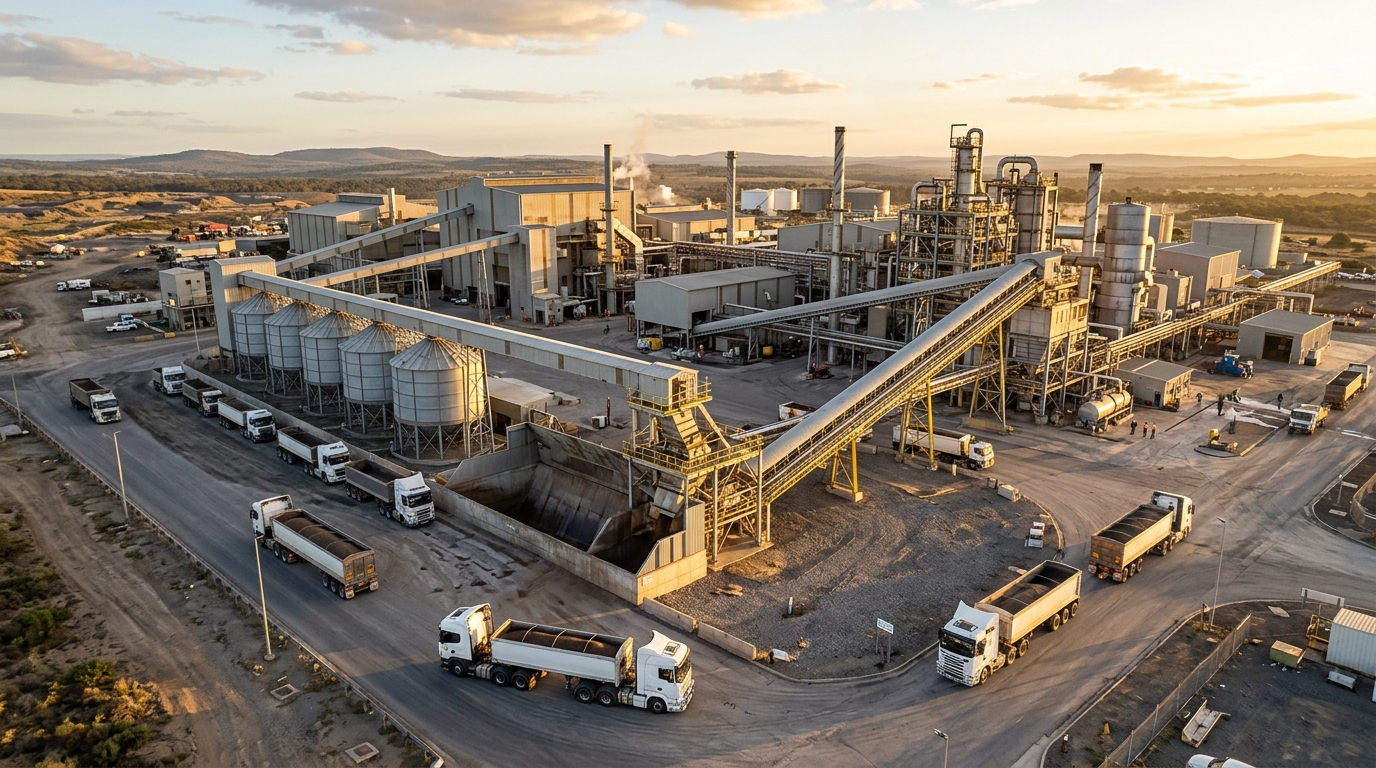
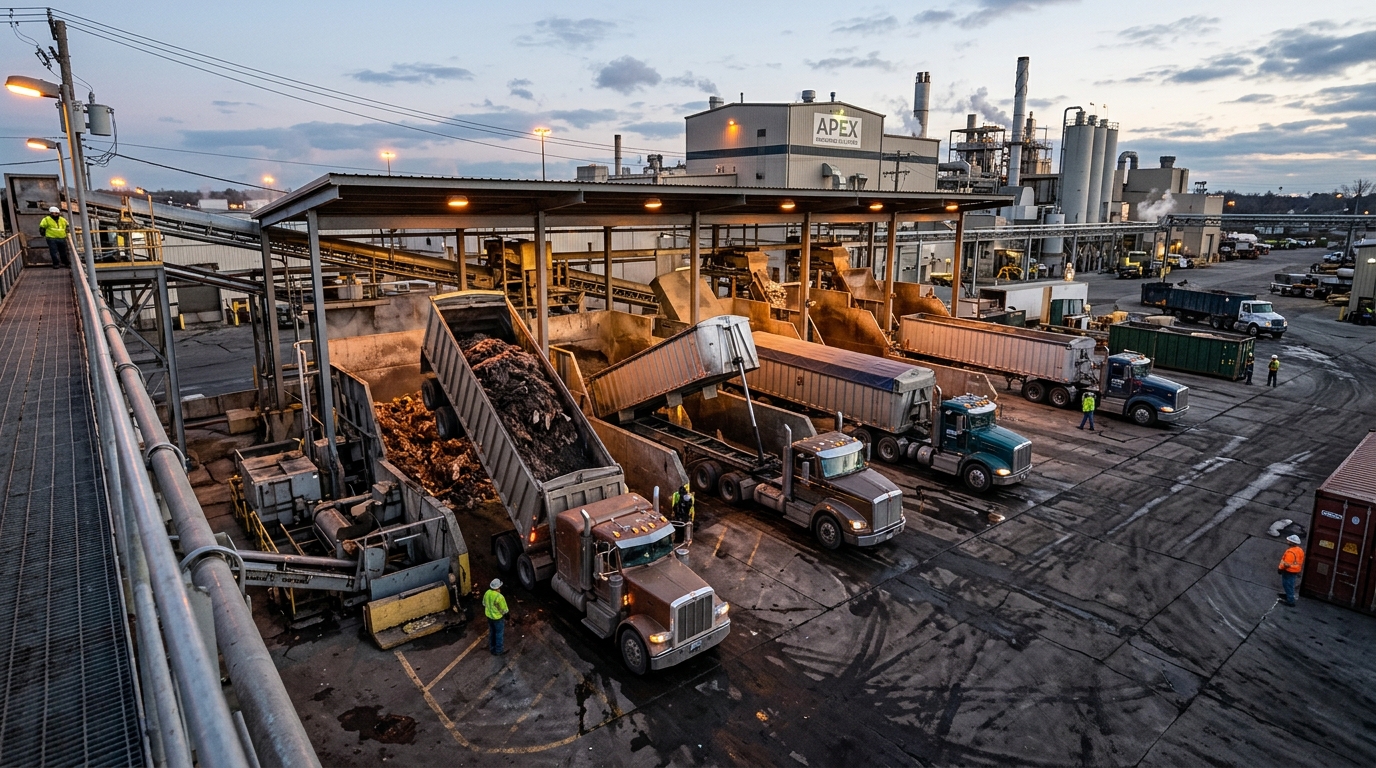
Trucks unloading variable volumes of raw material at a rendering plant dock
The Buffer Bin: Your First Line of Defense
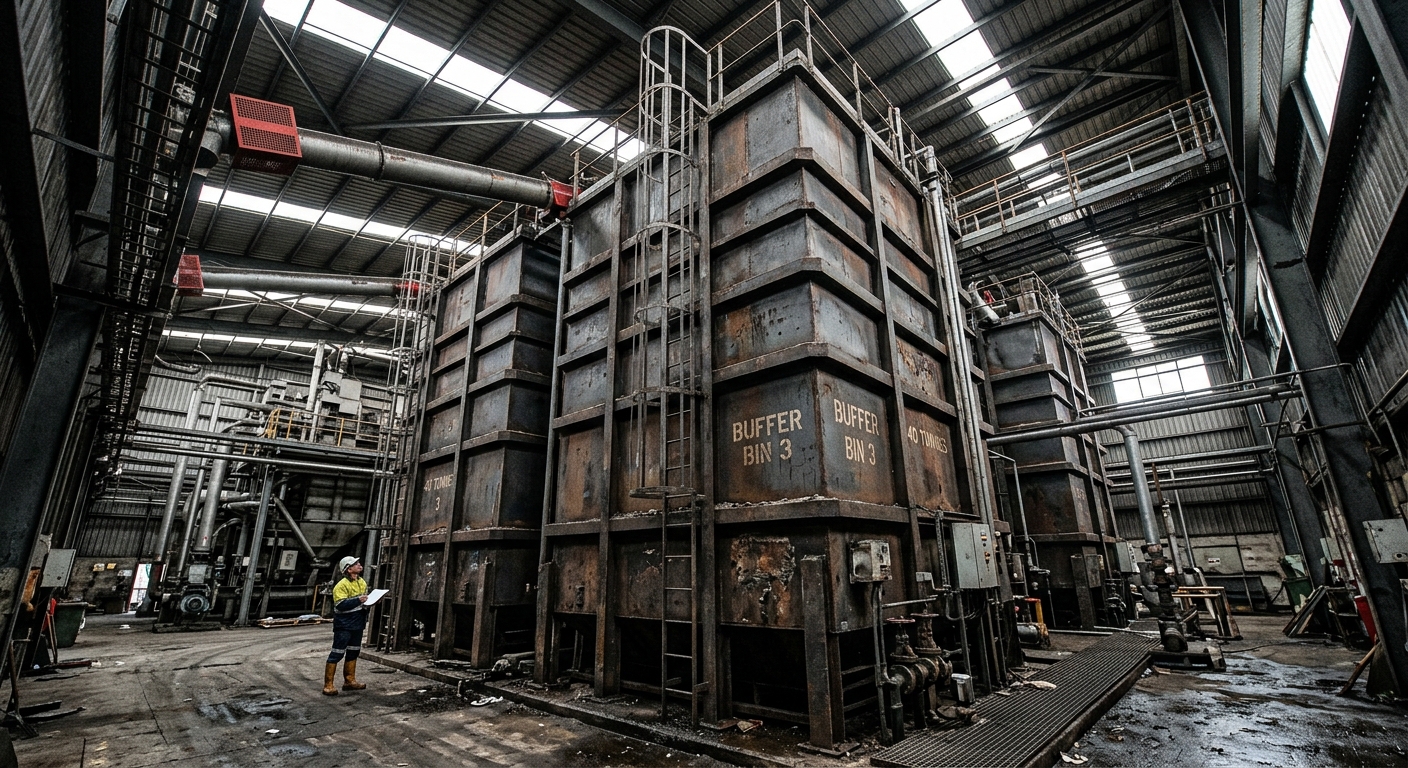
If there’s one piece of equipment that separates plants that handle load swings gracefully from plants that panic, it’s the buffer bin. A properly sized buffer bin system absorbs the difference between intake rate and processing rate, so a surge day doesn’t mean raw material sitting in open trucks or piling up on the dock.
Sizing Rule of Thumb
Most plants undersize their buffer capacity because they design around average daily volume instead of peak volume. A better rule: size your buffer bins to hold at least 1.5x your busiest single-shift intake. That extra half-shift of headroom is what keeps your cooker running at a steady rate even when the trucks keep coming.
For plants also dealing with intermittent overflow — say, an unexpected double shipment — a secondary buffer bin paired with overflow logic prevents the classic scramble of diverting material to unrefrigerated holding areas, which is a fast track to odor and quality complaints.
Large steel buffer bins used to manage raw material load variability in a rendering facility
Conveying Systems That Can Speed Up or Slow Down
A fixed-speed conveyor is fine until the day your intake doubles — then it becomes the bottleneck nobody planned for.
Belt vs. Screw: Which Flexes Better?
This is where the choice between a powered belt conveyor and a screw conveyor actually matters for variable loads. Belt conveyors handle bulk surges better because they’re less sensitive to material consistency changes — wet blood-heavy loads one day, drier feather stock the next. Screw conveyors are more consistent for metering exact rates but can jam if fed inconsistently sized material during a surge.
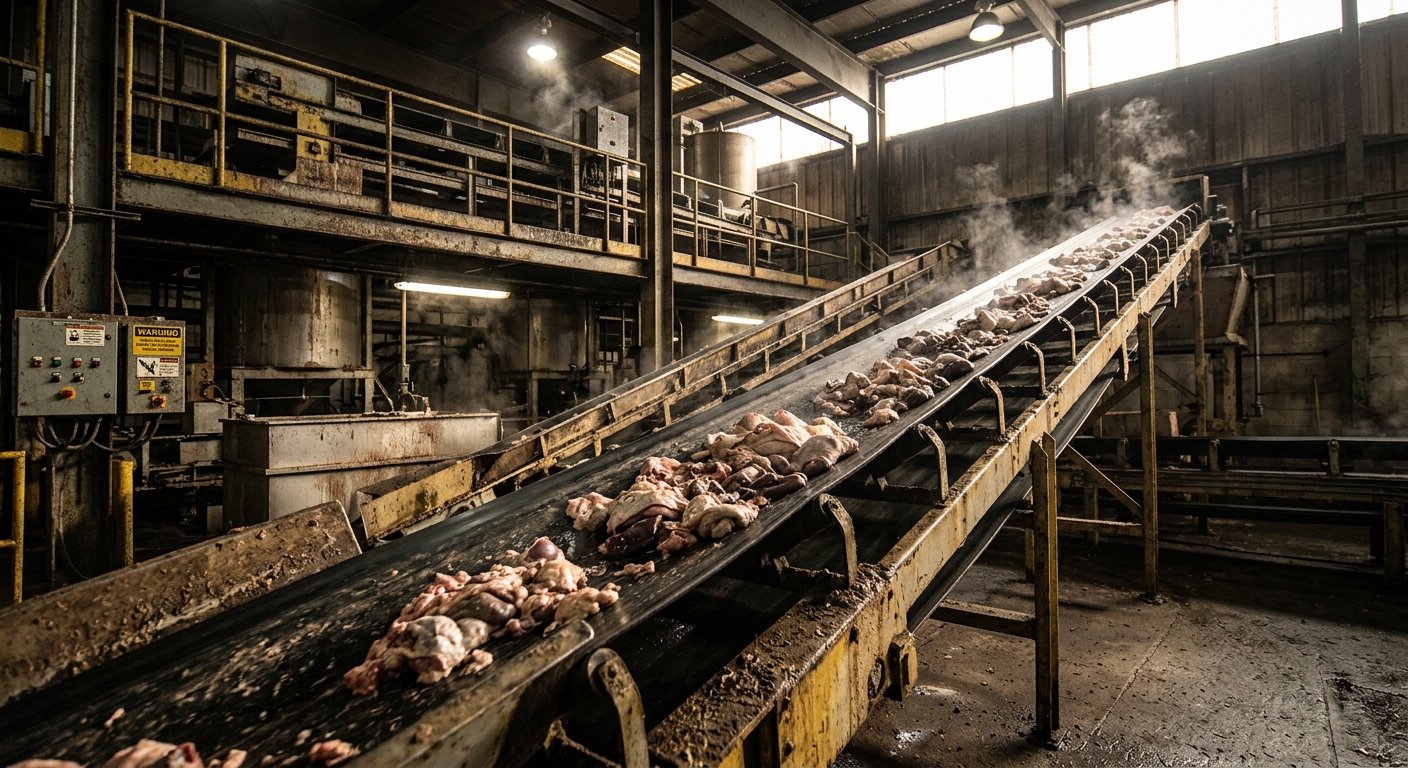
Powered belt conveyor transporting raw animal by-product material in a rendering plant
Batch vs. Continuous Cookers Under Variable Load
Your cooking system choice directly affects how well you absorb intake swings. Continuous cookers run best with a steady feed rate — they’re efficient, but they punish inconsistency. Batch cookers, by contrast, tolerate variable load better because each batch is a discrete unit; you can run more batches on a heavy day and fewer on a light one without disrupting the whole line.
We go deeper into the tradeoffs in our batch cooker vs. continuous cooker comparison, but the short version for variable-load plants: if your intake swings more than 30% week to week, batch systems generally give you more operational flexibility, even though continuous systems win on steady-state efficiency.
Odor and Compliance Risk During Surge Periods
Here’s a mistake plants make constantly: they assume odor issues only come from equipment, not from scheduling. Wrong. Raw material sitting too long during an intake surge — even for a few extra hours — accelerates decomposition and spikes hydrogen sulfide and ammonia emissions well before the material even reaches the cooker.Z
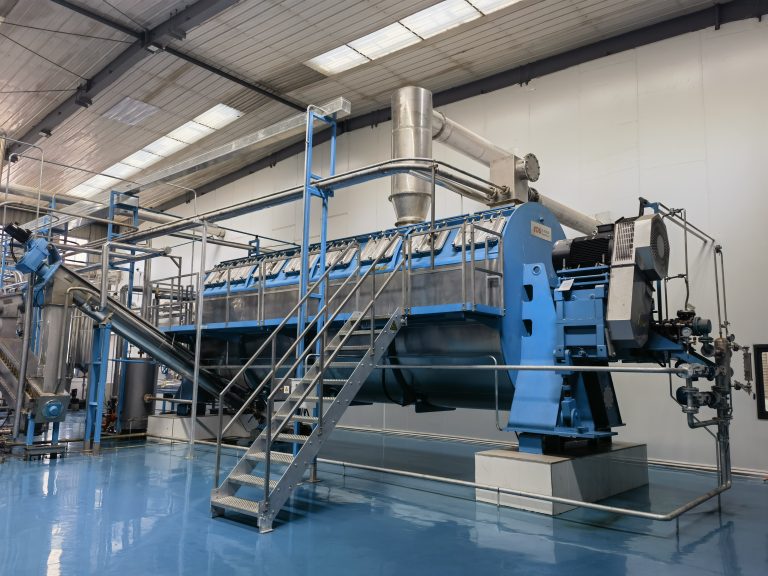
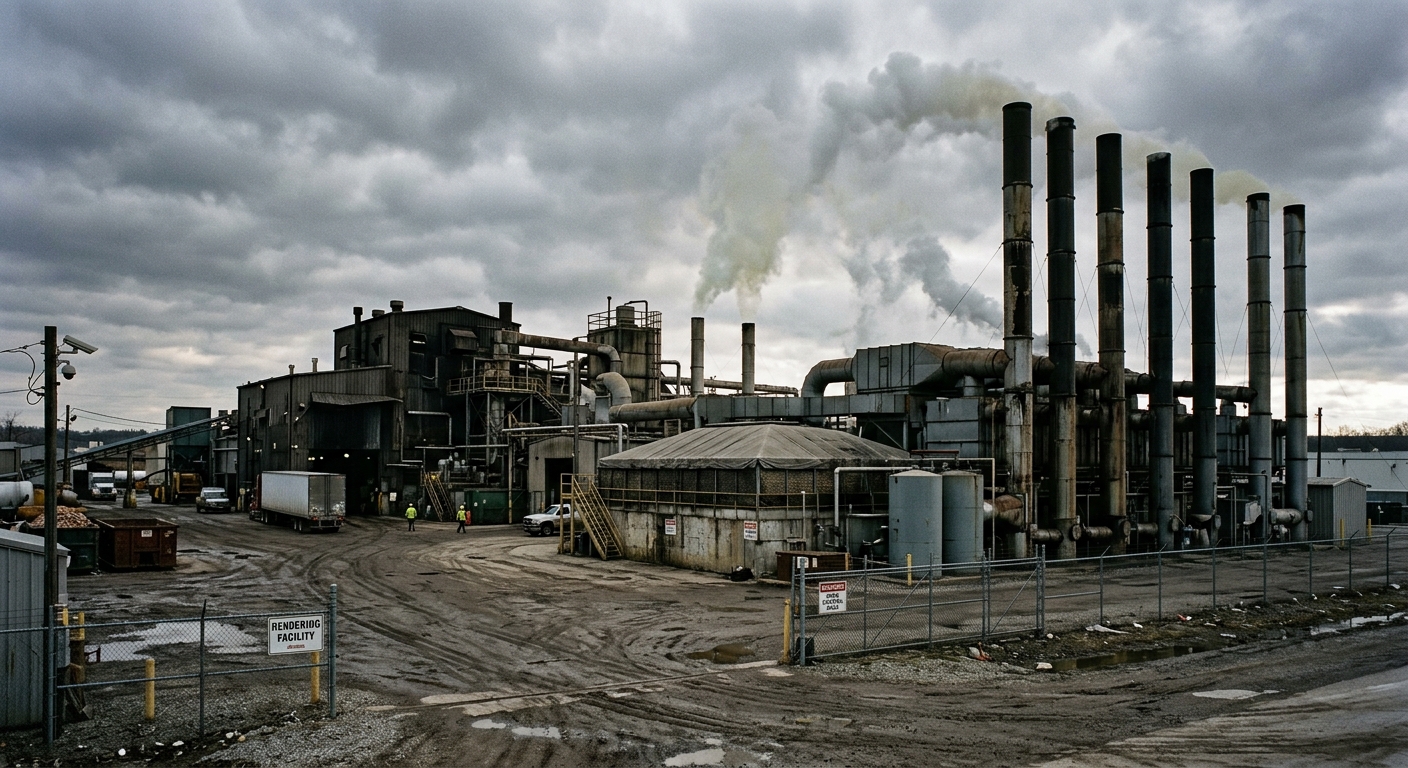
Rendering plant exterior with odor control equipment managing emissions during intake surges
Staffing and Scheduling: The Human Side of Variable Loads
Equipment gets all the attention, but a plant with perfect buffer bins and flexible conveying still fails if the crew isn’t scheduled around known intake patterns. Most rendering plants know their high-volume days weeks in advance — slaughterhouse kill schedules, seasonal fish catch reports, feed mill delivery contracts. Yet a surprising number still staff every day identically.
Cross-training staff to shift between intake handling and downstream processing on surge days costs nothing but planning time, and it’s often the cheapest fix on this whole list. Combine that with a clear start-up and shutdown routine for adding or pulling extra batch runs, and you get a plant that flexes without needing new capital equipment at all.
When to Invest in More Capacity vs. Better Flexibility
Not every load problem needs a bigger machine. Before signing off on new equipment, ask: is this a capacity problem or a flexibility problem? If your plant genuinely can’t process your average monthly volume even with good buffering, you need more capacity — bigger cookers, more fish meal processing machine lines, or added conveying throughput.
But if the problem only shows up on peak days while average days run fine, that’s a flexibility problem — and throwing capital at bigger equipment often means overpaying for capacity you’ll rarely use. A raw material bin upgrade paired with smarter scheduling usually solves it for a fraction of the cost of a new processing line.

 Blog · 10 月 14, 2026 From Smart Ear Tags to Processing Records: The Data Chain the “15th Five-Year” Livestock Plan Wants to Connect Read More