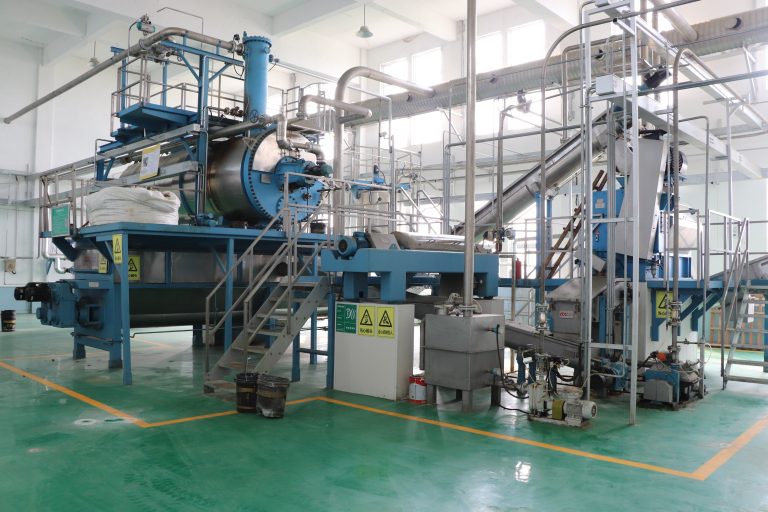
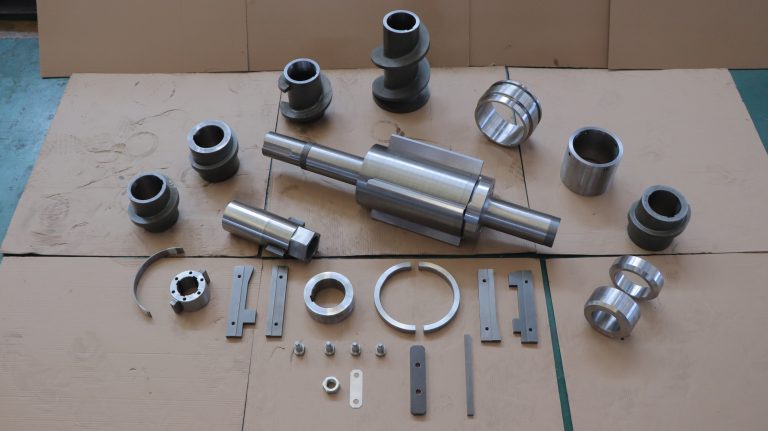
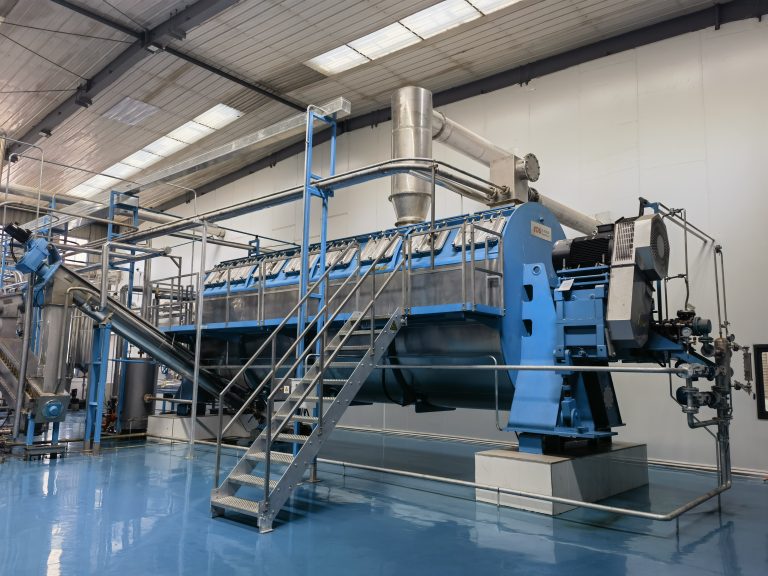
Plan spare parts for a rendering line by splitting your inventory into two very different buckets: critical spares (low-frequency, high-impact parts like gearboxes and main shafts that you must have on-site because a failure stops the entire line) and routine wear parts (high-frequency, low-cost items like hammer mill blades, screens, and seals that you consume on a predictable schedule). Get this split wrong — either overstocking wear items or under-stocking critical spares — and you’re either tying up capital in a parts closet or watching a $60,000-a-day plant sit idle waiting on a bearing housing from overseas. The fix isn’t complicated, but it does require actually looking at your failure history instead of guessing.
Why Most Plants Get This Split Backwards
Here’s the mistake we see constantly: plants stock five spare screen meshes but zero spare gearbox bearings. Why? Because screens are cheap and easy to order, so it feels responsible to keep extras. Gearboxes are expensive, so they get postponed — ‘we’ll order one if it breaks.’ That logic is exactly backwards.
The real question isn’t ‘what’s cheap to stock,’ it’s ‘what stops production if it fails, and how long would I wait for a replacement?’ A screen mesh failure is annoying but survivable — you can often run degraded for a shift. A cracked gearbox housing on a continuous rendering line means the whole cook-press-dry sequence stops, full stop, until that part arrives.
Rendering plant maintenance shop with gearboxes and bearings stored on metal shelving
Critical Spares: What Actually Belongs on This List
A critical spare is any part where downtime cost plus lead time makes stocking it non-negotiable. Run the math: if a part takes 8 weeks to source and your line generates $50,000/day, a single stockout can cost more than five replacement units combined. That’s the test.
Main drive gearboxes on cookers, presses, and dryers — often 6-12 week lead times for custom ratios
Screw press main shaft and cage assembly — machined to tolerance, rarely stocked by generic suppliers
Hammer crusher rotor shaft and bearing housing — see our breakdown of hammer crusher performance factors for why these wear at different rates depending on feedstock
Vacuum pump rotor assembly — critical to cooker cycle time; explained further in our vacuum pump station overview
PLC modules and drive inverters — electronics fail without warning and are almost never stocked locally
Routine Wear Parts: Stock by Schedule, Not by Guess
Wear parts don’t fail suddenly — they degrade. That means you can (and should) stock them based on consumption rate, not emergency instinct. If your hammer mill blades wear down every 400 operating hours, order the next set at 300 hours. Don’t wait for the metallic ring that tells you they’re already gone.
The Usual Suspects
Hammer mill blades and liner plates — replace on a running-hours schedule, not calendar time
Mechanical seals, gaskets, and O-rings — cheap, but a missing seal on a tallow storage tank valve can cause a product loss far exceeding the part cost
Keep 3-6 months of these on the shelf. They’re cheap, they’re standard catalog items, and running out of them for even a week creates cascading problems — a clogged screen backs up the whole cooker line just as badly as a broken gearbox, it just shouldn’t happen because you can see it coming.
The Middle Category Nobody Talks About: Semi-Critical Parts
Not everything fits neatly into ‘critical’ or ‘routine.’ There’s a third bucket that trips up even experienced plant managers: parts that aren’t consumed on a predictable schedule, but also aren’t catastrophic if you wait a few days for them.
Think cyclone dampers, sensor probes, small pumps, and instrumentation. These fail unpredictably like critical spares, but a 3-5 day wait is usually tolerable if you have workaround procedures. The smart move here is regional stocking — keep one unit at a distributor or shared warehouse rather than on every plant floor. It cuts carrying cost without exposing you to 8-week waits.
Building Your Parts List: A Practical Method
Skip the generic templates. Build your list from your own failure history — it’s the only data set that reflects your actual feedstock, your actual line speed, and your actual wear rates.
Four Steps That Work
Pull 24 months of maintenance logs. Rank every unplanned stoppage by hours lost, not by how memorable the failure was.
Tag each part by lead time. Anything over 3 weeks lead time automatically qualifies for critical-spare review, regardless of price.
Calculate downtime cost per hour. Multiply against expected failure frequency to get a real stocking-priority score — not a gut feeling.
Cross-check against your equipment supplier’s recommended spares list. Manufacturers know their own failure statistics better than any generic industry list, so use it as a baseline and adjust from your own logs.
Storage and Rotation: Where Plants Waste Money
Buying the right spare and then letting it sit in a humid warehouse for three years is its own kind of failure. Bearings develop corrosion pitting. Rubber seals dry out and crack. Electronics degrade from moisture even in sealed boxes.
Rotate critical spares into a first-in-first-out system if they have shelf life (seals, gaskets, belts)
Store bearings and shafts with anti-corrosion coating in climate-controlled space, not an open shed
Label everything with the equipment serial number it fits — a mismatched part during an emergency is as bad as no part at all
A batch cooker line and a continuous cooker line don’t have the same spare parts profile — not close. Batch systems have simpler mechanical paths but more valve and actuator cycling, which shifts wear toward valve seats and pneumatic components. Continuous lines put more stress on drivetrain components running 24/7, shifting critical-spare priority toward gearboxes and bearings. If you’re still deciding between the two, our comparison on batch cooker vs. continuous cooker systems breaks down the mechanical differences that drive this.


 Blog · 10 月 14, 2026 From Smart Ear Tags to Processing Records: The Data Chain the “15th Five-Year” Livestock Plan Wants to Connect Read More